Welding inspection and NDT
IWI-S welding inspection and level 2 NDT (VT, PT, MT, UT) on pressure equipment, piping, forgings and structures.
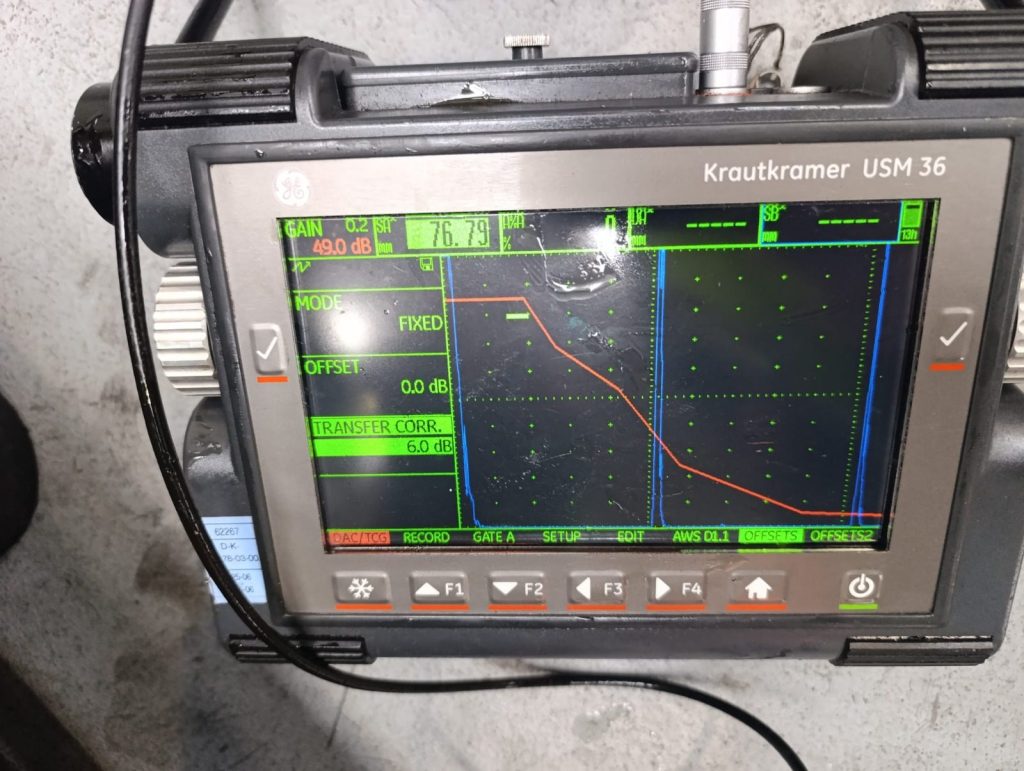
Welds checked against the procedure
I review the WPS and PQR before welding starts, inspect the welds visually and with NDT, and check that the NDT and heat treatment records match the parts.
Findings are reported with photographs and, where needed, an NCR that is followed through until it is closed.
IWI-S, ISO 9712, ASME, API
What I check
- Before weldingWPS and PQR reviewed against the project code and specification.
- Visual inspectionWeld profile, size and surface defects, to ISO 9712 level 2 (VT2).
- Surface NDTPenetrant (PT) and magnetic particle (MT) testing, level 2.
- Volumetric NDTUltrasonic testing (UT) of welds, forgings and bars, level 2.
- RecordsNDT reports and heat treatment records checked against the parts and the MTC.
Typical equipment
- Pressure vessels
- Shell and tube heat exchangers
- Valves and pipe spools
- Forgings, shafts and bars
- Structural steel
Codes and standards
- IWI-S (IIW)
- ISO 9712 for NDT personnel
- ASME and API, as specified by the project
Instruments
Ultrasonic flaw detector, magnetic yoke, penetrant kits, UV lamp and light meter, magnifiers and weld gauges.
- Ultrasonic testing
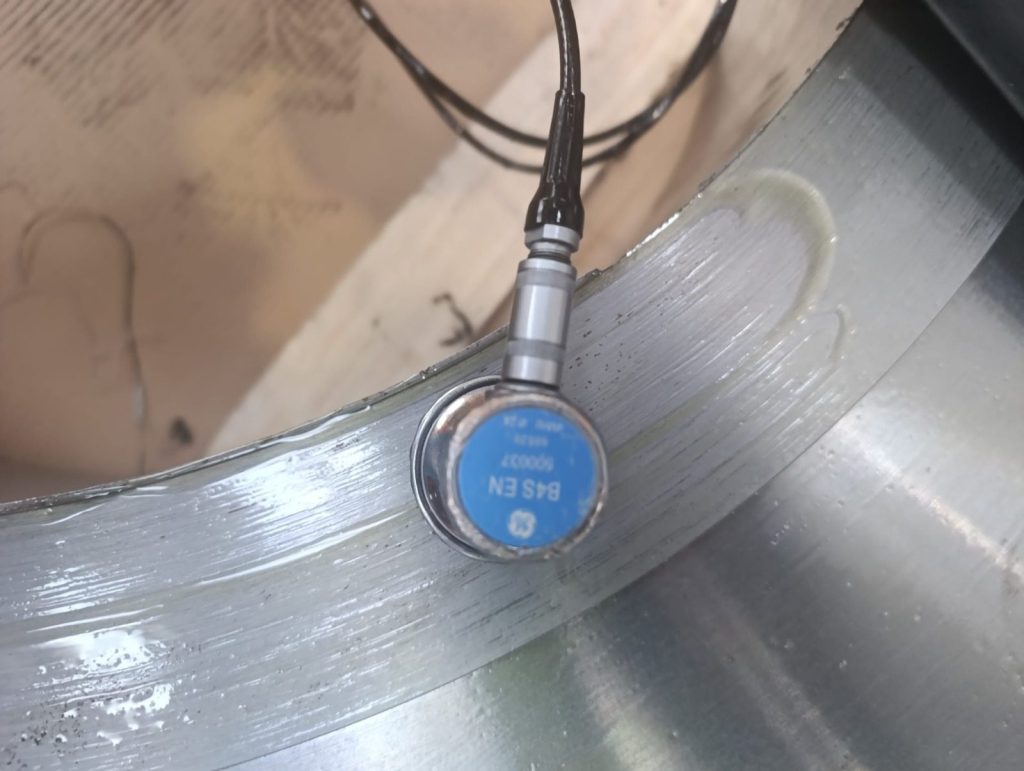 UT on a forging
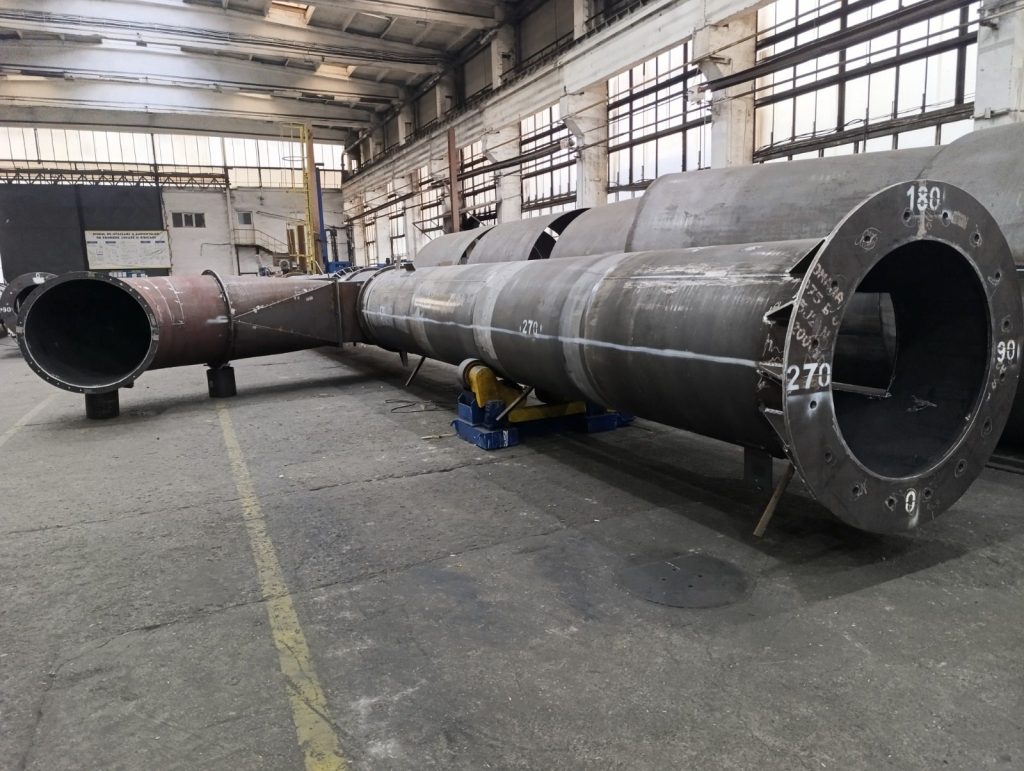 Welded fabrication
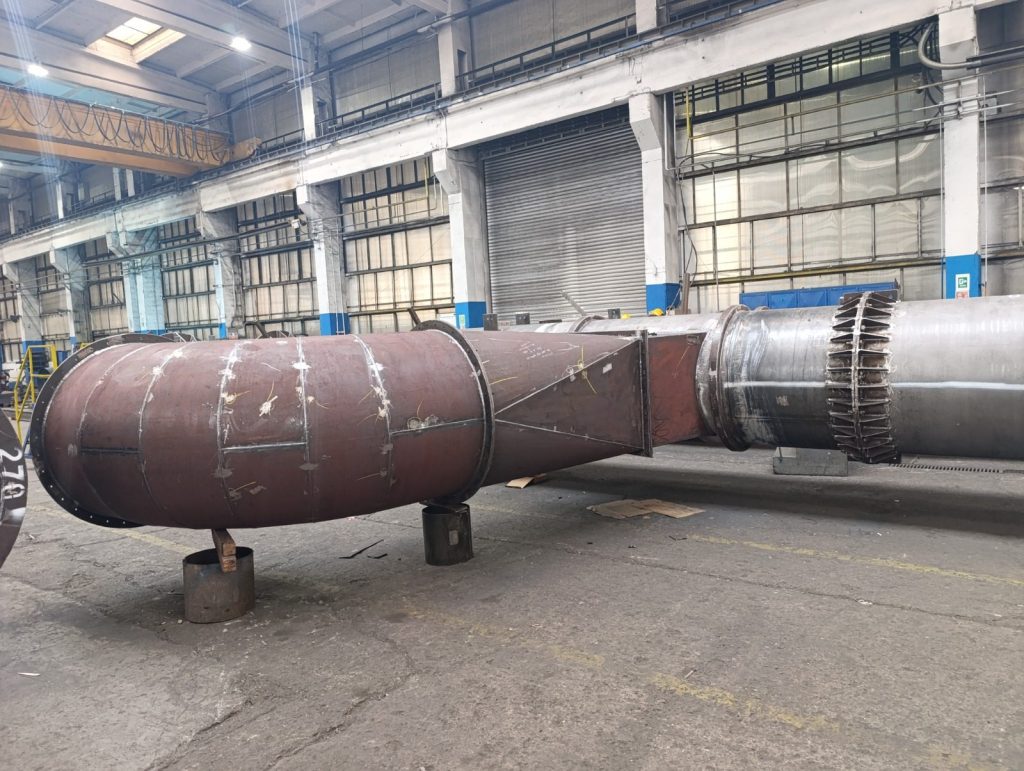 Pipe spool
Certifications for this work
- IWI-SInternational welding inspector, standard levelISIM Timișoara, 2026
- ISO 9712 VT2Visual testing, level 2ISIM Timișoara, ID 1874
- PT, MT, UT 2Penetrant, magnetic particle and ultrasonic testing, level 2AROEND
Need an inspector on site?
Send the location, dates and inspection scope, and I will confirm availability.
Or email barbu.constantin.alin@gmail.com